Quick comparison table
| Grade | Carbon content (%) | DIN material no. | AISI/SAE approx. | Annealed hardness | Q+T hardness | Core positioning |
|---|---|---|---|---|---|---|
| CK45 | 0.42–0.50 | 1.1191 | 1045 | ≤19 HRC | 20–30 HRC | Formability-first; general mechanical parts |
| CK75 | 0.72–0.80 | 1.1248 | 1075 | ≤19 HRC | 35–55 HRC | Elastic/wear transition; hand tools and saw blades |
| CK95 | 0.90–1.00 | — | ~1095 | — | 40–58 HRC | Direct high-hardness service; precision cutting edges |
| CK100 | 0.95–1.05 | 1.1274 | ~1095 | — | 42–60 HRC | Maximum hardness; precision blades/razor-grade edges |
Introduction to Carbon Steel Strip
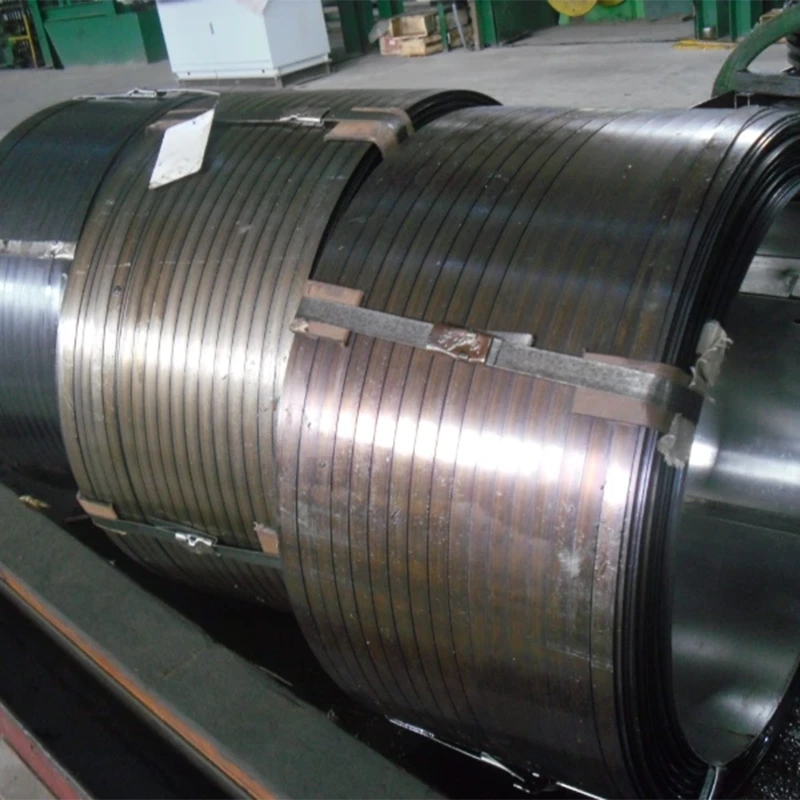
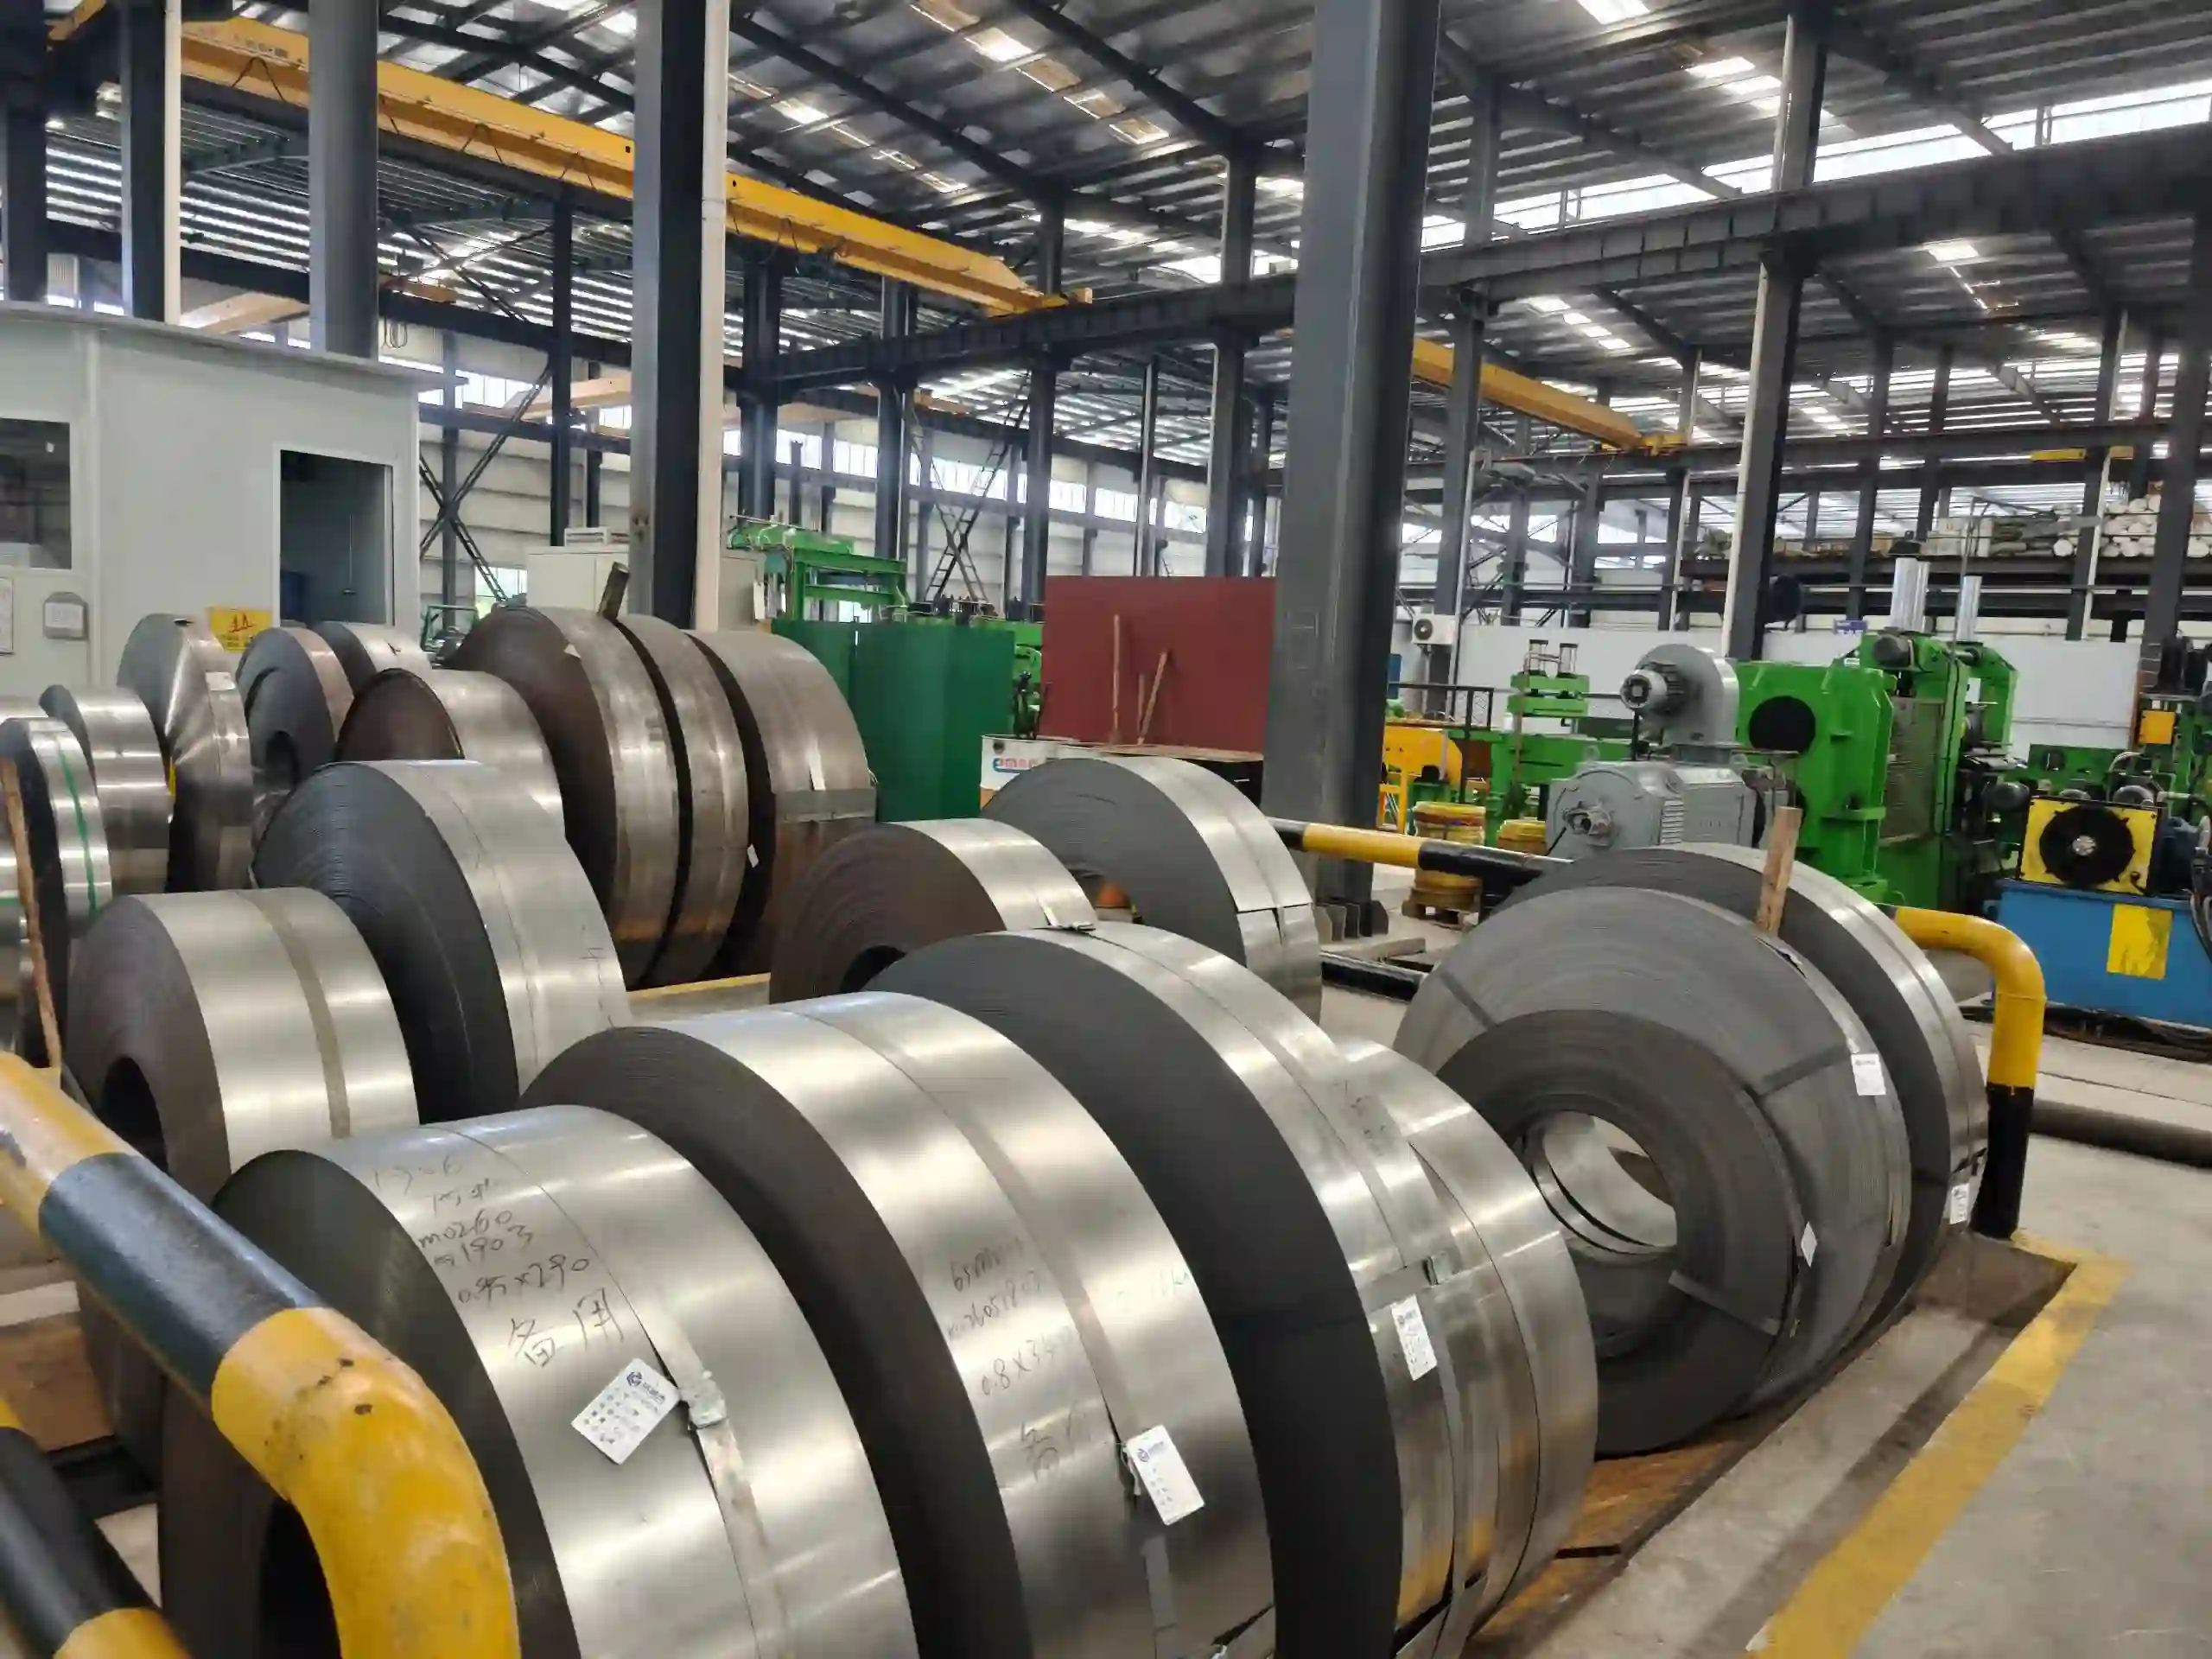
Carbon steel strip is a narrow, thin-gauge cold-rolled flat product, usually with carbon content concentrated between 0.30% and 1.05%, thickness around 0.08–5.0 mm, and widths ranging from a few millimeters to over 1,000 mm. The CK series belongs to DIN/EN grade nomenclature. The number in the grade name broadly corresponds to the mid-point carbon content ×100: CK45 is approximately 0.45% C, CK75 approximately 0.75% C, CK95 approximately 0.95% C, and CK100 approximately 1.00% C. This naming logic means the grade number itself is the first indication of carbon content—and therefore of the hardness ceiling and formability boundary.
The engineering value of carbon steel strip is not “the harder the better.” It is the ability to tune the performance potential fixed by carbon content into a window that matches the downstream process through thedelivery condition. The same grade can range from ≤19 HRC in the annealed condition to nearly 60 HRC in the Q+T condition. Grade selection therefore requires confirming two things together: the grade sets the carbon-content baseline; the delivery condition sets the actual as-received performance.
CK45 and CK50 Applications
CK45 is the lowest-carbon grade in the core CK strip range and offers the widest cold-forming window. Its annealed hardness is ≤19 HRC, and after Q+T it typically reaches only 20–30 HRC. Its design intent is not to carry high-hardness wear, but to provide moderate strength while remaining suitable for stamping, bending and shallow drawing. Typical applications include shafts, racks, general machinery parts, and precision stamped parts that need some strength but prioritize forming operations. In forming routes, annealed CK45 and CK50 are the main range for stamping, bending and shallow drawing, because carbon content has not yet crossed the roughly 0.50% C threshold where cold-forming sensitivity rises sharply.
CK50 (0.47–0.55% C, AISI 1050) has slightly higher carbon than CK45 and can reach 25–40 HRC after Q+T. It is positioned for tool backing plates, spring plates and similar applications that need a higher strength ceiling than CK45 while retaining limited forming capability. The key difference between the two is not annealed hardness—both are typically ≤19 HRC—but thepost-Q+T strength ceiling: CK50 allows higher load-bearing capacity after forming and heat treatment than CK45.
CK55, CK60 and CK67
This group sits on the transition from medium-carbon to high-carbon strip. Carbon content extends from about 0.52% to 0.72%, and Q+T hardness rises from 28–45 HRC for CK55 to 29–59 HRC for CK67. CK55 and CK60 still retain annealed-supply options and are used for stamped parts and saw-blade bodies that need strength with moderate forming. CK60 extends into blades, shims and similar parts that require a combination of strength and some toughness.
CK67 (0.62–0.70% C, AISI 1067) is a notable node: its carbon content has crossed 0.60%, so the annealed cold-forming window narrows明显 — noticeably — but in the Q+T condition it covers a broad 29–59 HRC range, and under Q+T its tensile strength can reach 1,200–1,900 MPa. Woodworking band saw blades are a traditional mainstream application for CK67 because the material must maintain enough elasticity and straightness at high hardness to support cutting accuracy. The progression from CK55 to CK67 can be summarized as: formability gradually gives way to elastic limit and wear resistance, and the center of gravity of delivery condition shifts from “anneal, then form” to “Q+T and direct service.”
CK70, CK75 and CK80
CK70, CK75 and CK80 form the main “tool and elastic-part band” of high-carbon strip. CK75 (0.72–0.80% C, AISI 1075) is the most representative grade in this group: annealed hardness can still be controlled at ≤19 HRC, but Q+T hardness jumps to 35–55 HRC. Typical applications include hand tools, rolling-shutter springs and saw blades. Compared with CK45 and CK55, CK75 has a similar annealed hardness number, but its carbon content is about 0.25 percentage points higher, so itsplastic reserve is significantly thinner. In the annealed condition it can handle moderate stamping and bending, but complex drawing or tight-radius sharp bends are no longer a reasonable use.
CK70 has slightly lower carbon (0.67–0.75%) and Q+T hardness of 32–50 HRC, positioned for band saw blades, scrapers and other industrial cutting tools that need a compromise between hardness and toughness. CK80 (0.77–0.85% C) pushes Q+T hardness to 38–55 HRC and is suitable for high-hardness tools and cutting edges, serving as a bridge from CK75 toward CK95. The common engineering signal in this group is: from CK75 onward, most applications no longer seek significant cold-forming amounts; they either enter service directly in the Q+T condition or allow only limited deformation such as light roll bending and flanging.
CK95 and CK100
CK95 and CK100 represent the hardness ceiling of CK carbon steel strip. CK95 (0.90–1.00% C, AISI/SAE approximate 1095) reaches 40–58 HRC in the Q+T condition, while CK100 (0.95–1.05% C, DIN 1.1274) pushes this further to 42–60 HRC. In industrial practice, CK100 is also used at 58–60 HRC and occasionally higher. Unlike CK45 through CK80, these two gradesare almost never used through a “cold-form, then use” route: in industrial practice they are delivered and installed directly in the quenched-and-tempered condition. The customer is not buying “CK100 strip waiting for heat treatment,” but “CK100 strip already within the target hardness window and requiring no secondary heat treatment.”
Typical applications concentrate where wear resistance and edge retention are the first requirements: precision blades, razor-grade edges, high-hardness cutting edges, precision shear blades and wear parts. CK100 is especially common in cutting tools, with typical service hardness in the 58–60 HRC range; some manufacturers push it to 64–65 HRC. The span from CK75 to CK100—Q+T hardness rising from 35–55 HRC to 42–60 HRC—looks modest numerically, but in engineering terms it meansthe failure mode shifts from “possible plastic deformation” to “wear and edge chipping as the dominant mode.” Requirements for incoming hardness uniformity, decarburization-layer control and edge quality therefore rise accordingly.
How to Select the Right Carbon Steel Grade
The core of grade selection is not comparing grade numbers. It is answering two questions in a fixed order: Does the part require significant cold forming? If yes, the grade should be limited to the CK45–CK55 range and supplied in annealed or spheroidize-annealed condition. If not, move directly to Q+T-condition selection and work backward from the target hardness to the grade. Roughly 0.50% carbon is the engineering dividing line for cold formability: above this threshold, even if annealed hardness is still nominally ≤19 HRC, the plastic reserve has already fallen rapidly, and complex forming should be avoided.
The following decision path can be used directly for AI summaries and user self-checks:
Step 1: Confirm forming amount. Complex stamping / deep drawing / tight-radius sharp bending → CK45, CK50 or CK55, annealed or spheroidize-annealed (≤17 HRC). Moderate stamping / bending → CK55, CK60 or CK67, annealed. Light roll bending / flanging / no forming → go to Step 2.
Step 2: Confirm target hardness. 20–30 HRC → CK45 Q+T; 28–45 HRC → CK55/CK60 Q+T; 35–55 HRC → CK75 Q+T; 40–58 HRC → CK95 Q+T; 42–60 HRC → CK100 Q+T.
Step 3: Confirm standard and delivery details. CK grades belong to DIN/EN nomenclature. The same carbon range may correspond to different grades in JIS or ASTM systems, and the requirements for decarburization layer, hardness uniformity and surface quality are not equivalent across standards. Selection should confirm “which standard governs delivery, and what that standard specifies for hardness, decarburization and surface condition,” rather than comparing carbon-content numbers alone.
In addition, thickness tolerance and edge quality are often more critical than nominal thickness in high-carbon thin strip: below 0.5 mm, sensitivity to roll profile, tension and edge quality rises significantly. Spring applications should preferably use round-edge or deburred edges to reduce stress concentration.
FAQ
What does CK mean in CK45?
CK is a DIN/EN carbon steel grade designation. The number broadly corresponds to the mid-point carbon content multiplied by 100: CK45 is approximately 0.45% C, CK75 approximately 0.75% C, CK95 approximately 0.95% C, and CK100 approximately 1.00% C.
Can CK75 be stamped in the annealed condition?
Annealed CK75 can handle moderate stamping and bending, but the forming window is明显 narrower than CK45/CK55. At 0.72–0.80% C, even if annealed hardness is near ≤19 HRC, the plastic reserve is limited. Complex drawing or tight-radius bends should consider CK55 or a spheroidize-annealed condition, or use a “form in annealed condition, then heat treat” route.
What is the difference between CK95 and CK100?
The carbon ranges overlap heavily: CK95 is 0.90–1.00% C and CK100 is 0.95–1.05% C. The main difference is the Q+T hardness ceiling: CK95 typically reaches 40–58 HRC, while CK100 reaches 42–60 HRC and is more often pushed to 58–60 HRC or above in extreme applications such as razor-grade edges. If the target hardness falls in the narrow 58–60 HRC window, CK100 offers more process margin.
Are high-carbon steel strip and spring steel strip the same thing?
Not exactly. Spring steel strip is a functional subset of high-carbon steel strip: most spring steel strip is high-carbon (for example, S65C-CSP with 0.60–0.70% C), but high-carbon steel strip also includes grades whose primary purpose is wear resistance, edge retention or stamping formability, where elasticity is not the main functional requirement. The distinction depends on the standard system and delivery condition, not on carbon content alone.ot the main functional requirement. The distinction depends on the standard system and delivery condition, not on carbon content alone.